Highlight:
corn dryer machine low temperature
, grain dryer machine energy saving
, corn dryer machine cost efficient
Applicable Grains: |
Rice, Wheat, Corn, Soybeans And Other Granular Grains |
Heat Source: |
Air-source Heat Pump (auxiliary Electric Heating Optional) |
Moisture Reduction Range: |
5%~18% Adjustable |
Hot Air Working Temperature: |
40~60℃ Low-temperature Range, Intelligent Constant Temperature Control |
Moisture Control Accuracy: |
±0.5% |
Operating Ambient Temperature: |
-10℃~43℃ (auxiliary Heating Can Be Equipped For Low-temperature Environments) |
Tower Material: |
Hot-dip Galvanized Anti-corrosion Steel Plate |
Control System: |
Touchscreen Intelligent Automatic Control, Manual Mode Switchable |
Safety Configurations: |
Over-temperature Protection, Overload Protection, Grain Blockage Alarm, Fault Self-diagnosis |
Auxiliary Equipment: |
Online Moisture Detector, Multiple Access And Cleaning Hatches, Optional Tail Gas Dust Removal System |
Constant low temperature preserves grain quality green energy cuts costs and boosts efficiency
During peak grain harvesting seasons, large-scale grain depots, collection stations and post-harvest service centers are generally confronted with challenges in continuous grain drying. Traditional batch recirculating dryers require grain loading, recirculation and unloading, leading to operation interruptions between batches. Heat sources such as natural gas and biomass are plagued by environmental regulations, volatile fuel prices and grain contamination by flue gas. When high-moisture wet grain arrives in large quantities, insufficient processing capacity causes grain piling, overheating and mildew. Older continuous tower dryers adopt high-temperature direct drying, resulting in rice cracking, corn breakage, downgraded grain quality and price deductions from purchasers. In addition, open-flame heat sources bring fire hazards and heavy pressure from environmental inspections.
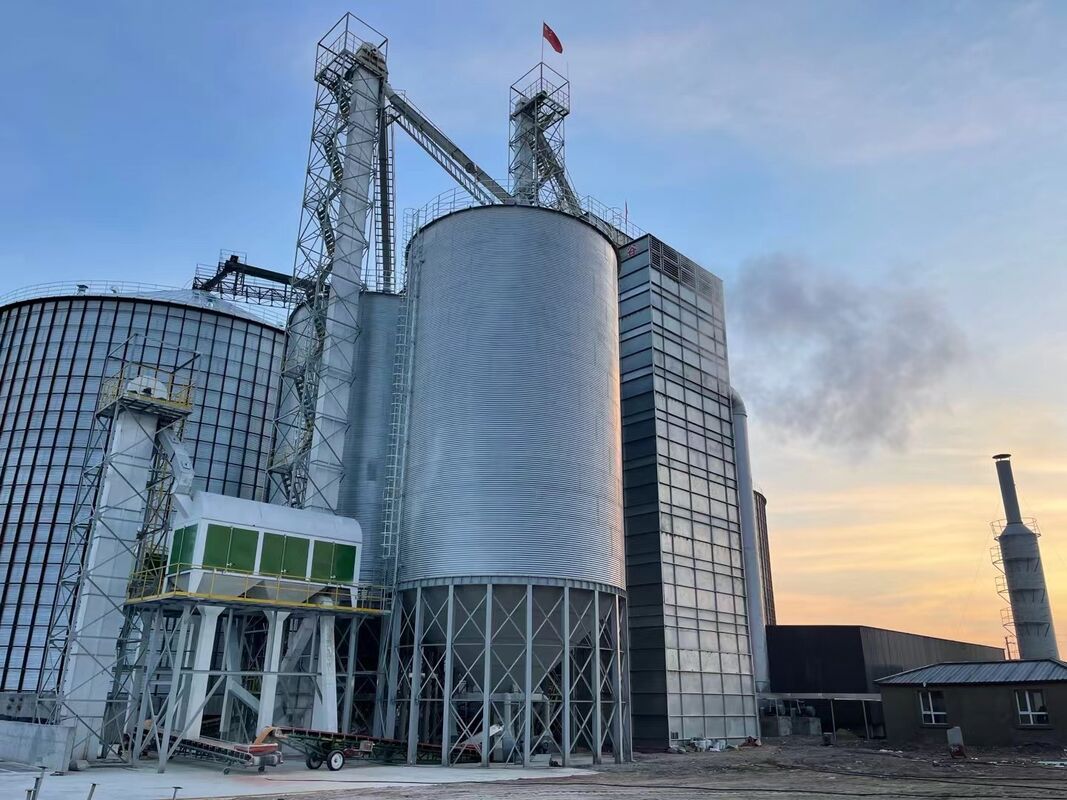
The WGH series continuous grain dryer developed by Zhengzhou Wangu Machinery is equipped with air-source heat pumps. Specially built for large-scale grain storage & collection facilities, post-harvest service centers and large cooperatives, it enables continuous grain feeding, drying and discharging. Adopting low-temperature heat pump technology, it balances high throughput, low operating cost, eco-friendliness and grain quality preservation, tackling the industry challenge of mass wet grain drying during harvest peaks.
Principle of Continuous Drying Process: Non-stop Assembly Line for Mass Wet Grain Operations
The WGH continuous dryer features an integrated structure of continuous downward drying and staged tempering. Wet grain is continuously delivered to the upper part of the tower by elevators and flows downwards by gravity, passing sequentially through the pre-drying section, main drying section, tempering section and cooling section. Clean low-temperature hot air generated by the heat pump penetrates the grain layer horizontally and removes grain moisture layer by layer. No batch loading or repeated grain recirculation is required; feeding and discharging run synchronously, supporting 24-hour non-stop operation.
A multi-layer angle-box air distribution structure inside the tower ensures even penetration of hot air. Grains across the full tower cross-section receive consistent heating to avoid local over-drying or under-drying. Staged tempering inside the tower allows internal grain moisture to migrate outward steadily after surface moisture evaporates, achieving uniform moisture reduction and preventing the phenomenon of dried grain surface with wet core. Once grains reach safe moisture content, they enter the cooling section for temperature reduction and are continuously discharged for direct conveying into silos. The whole process runs smoothly to process a steady stream of bulk wet grain without delays in harvest capture caused by batch switching during peak seasons.
Air-source Heat Pump Heat Source: Green Low-temperature Heating to Cut Energy Consumption and Environmental Risks
The heat source determines the drying cost and compliance for large-scale drying operations. The heat pump version of the WGH unit extracts low-grade heat from ambient air and compresses it to produce clean hot air. Grains have zero contact with combustion flue gas. There is no smoke, sulfur dioxide or nitrogen oxide emission, complying with strict local environmental regulations without complicated dust removal and desulfurization facilities.
Heat pumps operate in low-temperature heating mode with stable and controllable hot air temperature, preventing grain damage from temperature fluctuations of conventional heat sources. Compared with natural gas and biomass, heat pumps are free of constraints in fuel procurement, transportation and stockpiling. Without open flame, fire hazards in drying workshops are greatly reduced. In regions with off-peak or preferential electricity prices, heat pumps deliver prominent long-term operating cost advantages and hedge against fuel price hikes. Equipped with waste heat recovery, the system recovers heat from exhaust dehumidified air to further improve thermal efficiency and reduce energy consumption per ton of dried grain.
Many customers worry that low-temperature heat pumps cannot keep up with high-capacity drying. The WGH continuous tower adopts multi-stage drying and built-in tempering. The moisture reduction process is divided into different zones in the tower. Stable throughput is realized via continuous grain flow. Low temperature does not equal low output while grain quality is fully guaranteed.
Low-temperature Continuous Grain Protection Technology: Reducing Breakage and Cracking to Realize Premium Grain Value
Large-scale drying easily causes hidden losses. Intensive high-temperature drying sharply increases rice cracking rate and reduces head rice yield. Cracked corn kernels raise impurities, leading to price cuts by buyers. Seed grains may lose viability under high temperature and lose commercial value.
The WGH heat pump continuous dryer implements full-process low-temperature drying integrated with in-tower staged tempering and post drying cooling. Grains dehydrate slowly with a stable gradient of internal and surface moisture to mitigate thermal shock and greatly lower risks of cracking and breakage. Dried grain temperature is close to ambient temperature and can be directly conveyed into warehouses without secondary cooling. One unit adapts to multiple grains including rice, wheat, corn and soybeans, maintaining stable quality for commercial grain. By adjusting grain flow speed and hot air temperature, it can dry high-quality grain to boost grain premium and convert drying-related grain loss into tangible profits.
Stable Continuous Operation for Post-harvest Service Centers and Large-scale Grain Collection Scenarios
The WGH continuous heat pump grain dryer features continuous assembly-line operation, suitable for scenarios requiring large daily throughput and urgent grain processing in harvest seasons: grain post-harvest service centers, large grain depots, large-scale cooperatives and grain purchasing stations. Round-the-clock continuous operation in peak seasons enables immediate drying of incoming bulk wet grain and reduces mildew risks from wet grain stockpiling. The machine can steplessly adjust grain descending speed according to grain moisture and variety to adapt to variable incoming grain conditions and stabilize moisture compliance. The tower is made of anti-corrosion steel plates resistant to dust corrosion for reliable long-term continuous operation.
The dryer can be matched with front-end grain cleaning & elevating equipment and back-end silo conveying equipment to build a fully automated drying production line, cutting manual handling and labor costs.
Intelligent Control System, Simple Operation & Maintenance to Eliminate Downtime Risks for Continuous Production
Continuous production lines fear unexpected shutdowns most, which may lead to deterioration of massive wet grain. The WGH series is fitted with an online moisture monitoring system to track inlet and outlet grain moisture in real time and automatically adjust grain flow speed and heat pump hot air temperature. The machine adopts intelligent touch control with visualized parameters and supports switching between automatic and manual modes. The system has multi-protection against overload, over-temperature and water shortage. The heat pump unit comes with fault self-check and alarm functions.
Multiple access and cleaning ports are reserved on the tower for convenient daily impurity removal, maintenance and troubleshooting. The machine adopts a modular structure for easy disassembly and maintenance of key components. Optional dust removal system ensures qualified tail gas emission. The equipment has a low operation threshold and does not require many skilled operators on duty to reduce labor reliance.
odel Selection & Policy Support: Scientific Evaluation to Alleviate Equipment Investment Pressure
Zhengzhou Wangu WGH series continuous grain dryers have obtained agricultural machinery promotion certification. Purchasers can apply for national and local agricultural machinery purchase subsidies in accordance with regulations to ease upfront investment pressure. Five dimensions shall be evaluated for model selection:
- Estimate daily throughput and peak wet grain processing capacity in harvest seasons to match machine output.
- Determine grain flow speed and heat pump temperature parameters based on initial grain moisture and grain variety.
- Check power supply conditions of the plant, including transformer capacity, local electricity price and off-peak power policy to assess heat pump economy.
- Plan site layout and design routes for grain feeding, drying, discharging and warehousing.
- Confirm local environmental emission requirements and finalize the heat pump solution.
After defining working conditions, contact the technical team of Zhengzhou Wangu Machinery to customize a complete continuous drying solution and avoid overcapacity or insufficient configuration.

 Your message must be between 20-3,000 characters!